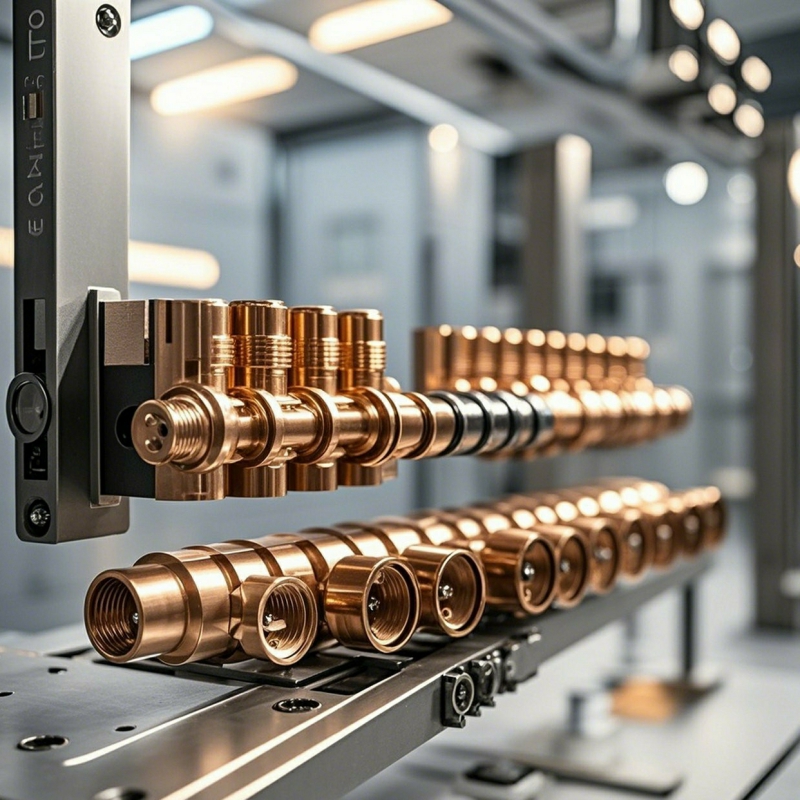
An electronics part fails in one of three ways: a contact surface oxidises until the contact resistance climbs and the connector runs hot; a housing develops a seam that lets radiated noise in; a moulded part wears through its finish and sheds particles. Electronics and telecommunications part coating addresses these mechanisms at the surface, and the film is chosen by whether the part needs conductivity, insulation, low friction or a combination.
The constraints are tighter here than in most industrial work. Parts are small, often moulded in plastic or machined from copper alloys soft enough to be damaged by heat, and production runs in batches where thickness consistency matters more than absolute thickness. A 200-800 nm film is the typical order of magnitude: thick enough to carry an abrasion load, thin enough to leave the original geometry and insertion force. A coated part shields only if the film is continuous and properly bonded.
Typical parts we coat
- Contact and connection parts: connector shells, pins and sockets, USB-C and Type-C contacts, PCB terminals, copper busbars
- Shielding and enclosure parts: shielding cans and covers, RF housings, antenna covers, radome and grounding brackets
- Radio-frequency and antenna parts: antenna reflectors, feed horns, array elements
- Consumer and mobile parts: mobile phone metal housings, notebook and tablet shells, 3C casings, bezels
- Optical and optoelectronic parts: fibre-optic connector bodies, filter frames, lens holders, window frames
- Thermal and composite parts: heat-spreader baseplates, graphite and carbon-fibre housings, plastic housings needing a conductive skin
Coating options and why they fit
Titanium nitride (TiN)
TiN is the default for contact and conductive surfaces, as both a conductor and a hard wear film. Typical Vickers hardness is 2300-2500 HV at 200-1000 nm, and the reported friction coefficient of 0.2-0.4 sits below the 0.5-0.7 of uncoated copper contacts. On a USB-C interface a TiN film has been reported to reduce insertion force by 25-35 per cent and to hold the contact resistance increase below 3 per cent over 10,000 cycles, against more than 10 per cent uncoated.
Aluminium nitride (AlN)
AlN serves housings and covers where heat has to be removed but current must not flow. Its thermal conductivity is about 320 W/m.K while it stays an insulator, and a single 3 micrometre layer is reported to deliver more than 30 dB of attenuation across 1-10 GHz. Deposition stays below 250 degrees Celsius, with an ABS bracket reported to warp under 0.05 mm.
Chromium nitride (CrN) and the diamond-like carbon family
CrN is the harder and more corrosion-resistant nitride, at 1800-2200 HV. On a shielding enclosure the reported shielding effectiveness is 90 dB or above, and a separate case reports it rising from 70 dB to 92 dB once the coated panel replaced the uncoated one. For rubbing surfaces the amorphous carbon films are the choice: the tetrahedral form of DLC (diamond-like carbon) is reported at 74.8-84.0 GPa with an sp3 fraction above 70 per cent, and the filtered arc process keeps deposition below 80 degrees Celsius.
Metal and composite films
For carbon-fibre, graphite and carbon-carbon substrates the film is a metal, because the substrate is not a uniform conductor. Silver reaches a sheet resistance of about 1 ohm per square, nickel 1-5 and aluminium 1-3, with a shielding effectiveness of 40-70 dB across 30 MHz-1 GHz at 0.5-5 micrometres. On a metal base, 2-4 ohm per square is the reference for antenna-grade TiN, 1.0-2.5 for aluminium.
How the process works
Pre-treatment, ion bombardment, deposition, post-treatment. For contact work, pre-treatment decides whether the film adheres at all: degreasing, a light chemical or plasma clean to remove the oxide, then argon ion bombardment inside the chamber that strips the last contamination and leaves the surface active. Parts are fixtured so the contact area is not marked.
Deposition is by arc ion plating for the compound films and MF magnetron sputtering where the surface finish has to be even over a large area, or where the substrate cannot take heat. Base vacuum is held at or below 5 x 10^-4 Pa, working pressure in the 0.2-2.0 Pa range, and a substrate bias of up to -1000 V keeps the film dense and adherent. Multilayer structures are deposited in one run, including an alternating TiN and AlN stack of 16 nanoscale layers within 1 micrometre reported to raise shielding to 70 dB at 18 GHz. Post-treatment adds sealing, thickness monitoring and a continuity inspection, because a pinhole defeats the shield.
What the numbers look like
- TiN on contacts, 2300-2500 HV at 200-1000 nm, a friction coefficient of 0.2-0.4 against 0.5-0.7 for uncoated copper, an insertion force reduced by 25-35 per cent, and a contact-resistance increase below 3 per cent over 10,000 insertion cycles
- TiN on copper terminals, a deposition temperature below 150 degrees Celsius, a thickness of 0.5-3 micrometres, and a contact-resistance increase 5 to 10 times smaller than bare copper after 1000 h at 85 degrees Celsius and 85 per cent humidity
- CrN, 1800-2200 HV, a shielding effectiveness of 90 dB or above on an enclosure, and a reported case of shielding rising from 70 dB to 92 dB once the coated panel replaced the uncoated one
- AlN, a thermal conductivity of about 320 W/m.K, more than 30 dB of attenuation from a single 3 micrometre layer across 1-10 GHz, a hardness of HV2000 or above, and salt spray above 500 h under ASTM B117
- DLC and ta-C, a reported hardness of 74.8-84.0 GPa with an sp3 fraction above 70 per cent, deposition below 80 degrees Celsius, and a reported elastic modulus of 750.8-829.7 GPa
- Metal films on carbon-fibre substrates, a sheet resistance of about 1 ohm per square for silver, 1-5 for nickel and 1-3 for aluminium, a shielding effectiveness of 40-70 dB across 30 MHz-1 GHz, and a thickness of 0.5-5 micrometres
- Multilayer shielding, 16 nanoscale TiN and AlN layers within 1 micrometre giving 70 dB at 18 GHz, and a composite Ti, Cu and AlN stack averaging 60 dB or better, reaching 80 dB on some geometries
Where this fits — and where it doesn’t
- Fits: contact surfaces needing a conductive, wear-resistant skin while keeping the mating geometry and insertion force, and housings, covers and brackets needing a continuous conductive skin for shielding, thermal spreading or grounding, in thin film rather than a plated shell
- Does not fit: a part that needs shielding but has no ground path, no seam treatment and no defined bond point. The film adds attenuation; the design supplies the return
- Does not fit: surfaces that will later be soldered, spot-welded or heavily bent. A 200-800 nm film is hard and brittle, and cracks when the substrate flexes
- Does not fit: high-current power joints where contact resistance must stay at bare-copper levels, where a precious metal contact plate is the usual answer
- Does not fit: moulded plastic housings that cannot tolerate 250 degrees Celsius, unless a low-temperature route below 80 degrees Celsius is developed
Frequently asked questions
What sheet resistance can be achieved, and does that give useful shielding?
It depends on the substrate and the film. On carbon-fibre and graphite substrates, silver reaches about 1 ohm per square, nickel 1-5 and aluminium 1-3, with a shielding effectiveness of 40-70 dB between 30 MHz and 1 GHz. For a compound film on a metal part, antenna-grade TiN is reported down to 2-4 ohm per square. The figure that matters is the one measured on the finished part.
Can a plastic housing be coated without distorting it?
Yes, and temperature is the controlling variable. A general run holds the substrate between 80 and 180 degrees Celsius, and a low-temperature route below 80 degrees Celsius is available for moulded parts; an ABS bracket is reported to warp under 0.05 mm. The plastic is plasma-activated before deposition, and the argon bombardment generates a nanostructured surface reported to lift adhesion threefold.
Does the coating affect signal integrity or insertion force?
It can, and this is worth settling before the order. A 400 nm TiN film on a Type-C contact is reported at an insertion loss below 0.1 dB at 10 GHz, and the same report gives an insertion force reduction of 25-35 per cent on a USB-C interface, which for a specified connector has to be checked against the mating partner’s rating. On RF housings the film raises shielding effectiveness but can add insertion loss, so the antenna budget needs review with the coating in place.
Send us a sample for a free coating feasibility assessment. Send the substrate and its surface condition, the function of the part, the frequency band or electrical specification it must meet, and the batch size. The first proposal comes back with the film system, a thickness range, the process temperature and an inspection plan.
Xi’an Zhiyang Baina Vacuum Coating Co., Ltd. | PVD vacuum coating services and coating technology cooperation for all types of parts. Samples welcome for a free coating assessment.
Address: Xi’an, Shaanxi, China